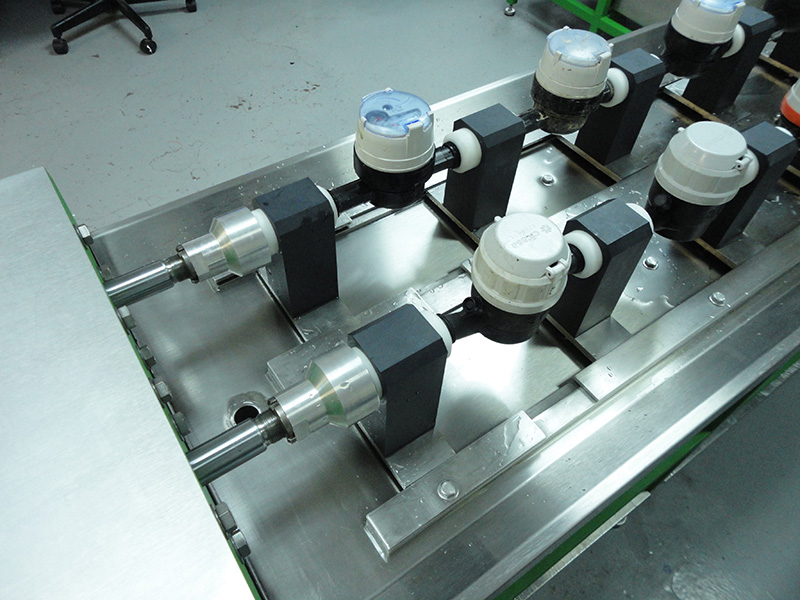
A water meter can pass calibration at the test bench and still create costly field problems if its housing, sealing surfaces, or internal geometry vary from part to part. Water meter optimization begins with controlling the plastic components that protect the measuring mechanism, manage water flow, and maintain a reliable connection for years of service.
For OEMs, utilities, and product developers, the objective is not simply to produce a molded body at the lowest piece price. It is to manufacture a repeatable component that supports measurement accuracy, withstands pressure and environmental exposure, installs correctly, and scales without unexpected quality drift. That requires product engineering, tooling discipline, material knowledge, and production control working together.
Water Meter Optimization Is a System Decision
A water meter housing looks straightforward, but its performance depends on a chain of tightly connected decisions. The internal chamber must guide water consistently around the measuring element. Threaded ports need to mate properly with fittings. O-ring grooves must create predictable compression. Cover interfaces, sensor cavities, and tamper-resistant features must remain dimensionally stable after molding and throughout the expected service life.
A small variation can have an outsized effect. Flash near a sealing feature may create a leak path. Warpage around a threaded connection can make assembly difficult. Shrinkage in a sensor pocket can affect the position of an electronic module. Even a cosmetic sink mark may indicate uneven wall thickness or poor packing in a location that also influences dimensional stability.
That is why optimization should be defined around functional outcomes: flow consistency, pressure resistance, sealing reliability, accurate component location, efficient assembly, and stable production yield. The right approach depends on the meter type, operating pressure, water quality, temperature range, installation environment, regulatory requirements, and planned production volume.
Start With the Critical Features, Not the Cosmetic Model
A manufacturable water meter component starts with a clear distinction between critical and noncritical dimensions. Critical features normally include inlet and outlet geometry, sealing grooves, mating faces, thread profiles, bearing locations, register interfaces, and surfaces that locate electronic or mechanical measurement assemblies. These features need defined tolerances, inspection methods, and a realistic understanding of molding variation.
Design teams sometimes apply very tight tolerances across an entire part drawing. This can raise tooling complexity and inspection cost without improving field performance. A stronger method is to reserve the tightest controls for features that affect fit, flow, leakage, and measurement. Less critical external surfaces can allow more variation, provided appearance and installation requirements are met.
Wall thickness deserves the same attention. Thick-to-thin transitions create uneven cooling, which can lead to sink marks, internal stress, and distortion. Uniform nominal walls, properly designed ribs, and gradual transitions support more consistent filling and cooling. In some cases, a minor design adjustment can remove a molding risk before steel is cut, avoiding repeated mold modifications later.
Select Materials for Service Conditions and Process Stability
Material selection is central to water meter optimization because the housing is exposed to more than water. Depending on the application, it may face pressure cycling, outdoor ultraviolet exposure, freezing conditions, disinfectants, minerals, installation loads, and temperature changes. The material must also mold consistently in the chosen geometry.
Engineering plastics such as reinforced polyamide, acetal, polypropylene, and specialty compounds may be considered based on the meter design. There is no universal best resin. A material with excellent stiffness may require careful management of moisture behavior. A chemically resistant material may present different challenges in creep resistance or thread performance. Glass reinforcement can improve strength and reduce shrinkage, but it can also affect surface finish, wear on tooling, and warpage behavior.
For potable water applications, material compliance requirements must be addressed early rather than treated as a final purchasing detail. The resin grade, colorant, additives, and any secondary components need to align with the applicable market and customer requirements. Changing a material after tooling is complete can alter shrinkage, gate performance, cycle time, and part dimensions.
The production question matters as much as the datasheet question. A material that performs well in a laboratory but has a narrow processing window can create avoidable scrap and inconsistency at volume. The preferred choice is one that satisfies the service specification while supporting stable, repeatable injection molding.
Tooling Determines Whether Performance Can Be Repeated
A high-quality mold does more than create the part shape. It controls the conditions under which every part is formed. Gate location influences flow direction, weld lines, pressure distribution, and fiber orientation in reinforced materials. Cooling layout influences cycle time, shrinkage, and warpage. Venting affects surface quality and the ability to fill detailed features. Ejection design prevents deformation of threads, sealing faces, and thin functional walls.
For water meter housings, mold design should also account for maintenance and expected production life. Replaceable inserts can be valuable around high-wear features or areas likely to require future revision. Slides, unscrewing mechanisms, or collapsible cores may be necessary for certain connection geometries, but each additional moving element introduces a maintenance consideration. The most sophisticated mechanism is not always the best solution if a simpler design can achieve the same functional result.
Mold flow analysis and design-for-manufacturing review provide the greatest value before fabrication. They allow the team to identify potential air traps, hesitation marks, high-pressure zones, or difficult-to-cool sections while changes are still fast and economical. Once production starts, data from first articles and pilot runs should be used to refine process settings and confirm that critical dimensions remain stable across the cavity layout.
Protect Accuracy Through Assembly Interfaces
The plastic housing does not measure water by itself, but it directly affects the components that do. Mechanical meters rely on controlled flow paths and stable locations for internal moving elements. Ultrasonic, electromagnetic, and smart meter designs may require precise sensor positioning, protected electronics, antenna clearance, or carefully managed internal cavities.
This creates a need for cross-functional design review. The molding team needs to understand which surfaces establish sensor alignment, where a gasket must seal, and how the meter will be assembled. The product team needs to understand draft requirements, parting lines, gate vestige, and realistic molding tolerances. When those disciplines work independently, problems tend to emerge during assembly or validation rather than during design.
Secondary operations should be considered early as well. Laser marking, ultrasonic welding, insert installation, leak testing, machining, and packing can all affect the final component. A part that is easy to mold but awkward to fixture, mark, or inspect may not be the most efficient production design.
Build Quality Control Around Real Failure Modes
Visual inspection alone is not enough for a functional meter housing. A capable quality plan connects inspection to the risks that matter in service. That may include dimensional checks on sealing features and threads, weight verification, pressure or leak testing, assembly-fit checks, and monitoring of critical process parameters.
Statistical process control is particularly useful when a dimension has a direct effect on sealing or alignment. Instead of waiting for a rejected batch, manufacturers can identify movement in the process before parts cross the specification limit. Cavity-specific measurement is also valuable in multi-cavity tooling because one cavity can begin to drift before the rest of the mold shows a clear issue.
Traceability should match the application risk and customer requirement. For high-volume utility products, lot records for resin, production date, process conditions, and inspection results support faster investigation if a field issue occurs. The goal is not paperwork for its own sake. It is the ability to isolate a problem, protect compliant inventory, and take corrective action without disrupting the entire supply chain.
Scale Without Losing Control
The transition from prototypes to repeat production is where many otherwise sound meter projects lose momentum. Prototype methods may prove the concept, but they do not always reveal the cooling, wear, cycle-time, or cavity-balance issues that appear at production volume. A production plan should define anticipated annual demand, desired number of cavities, automation opportunities, inspection frequency, and tooling maintenance intervals before launch.
An integrated manufacturing partner can reduce handoffs between product refinement, mold fabrication, molding, finishing, and quality verification. At Glasfil, in-house design and mold modification capability help teams respond quickly when pilot production identifies an issue that requires adjustment. This matters when a meter program must meet a fixed launch date while maintaining control of critical functional features.
Cost optimization should be evaluated across the full lifecycle. A lower-cost mold that produces inconsistent threads, requires frequent manual sorting, or creates higher leak-test failures rarely delivers genuine savings. The better investment is the one that supports predictable output, efficient assembly, and dependable field performance over the planned production run.
The practical next step is to review the water meter housing as a functional system: identify the features that protect measurement and sealing, validate the material against actual service conditions, and confirm that the tool can reproduce those features at volume. That early engineering discipline is what turns a molded component into a reliable part of the metering system.
Contact us to discuss your project, request a quotation, or arrange a technical consultation. Our team will help you determine the most cost-effective and reliable way to manufacture your part.