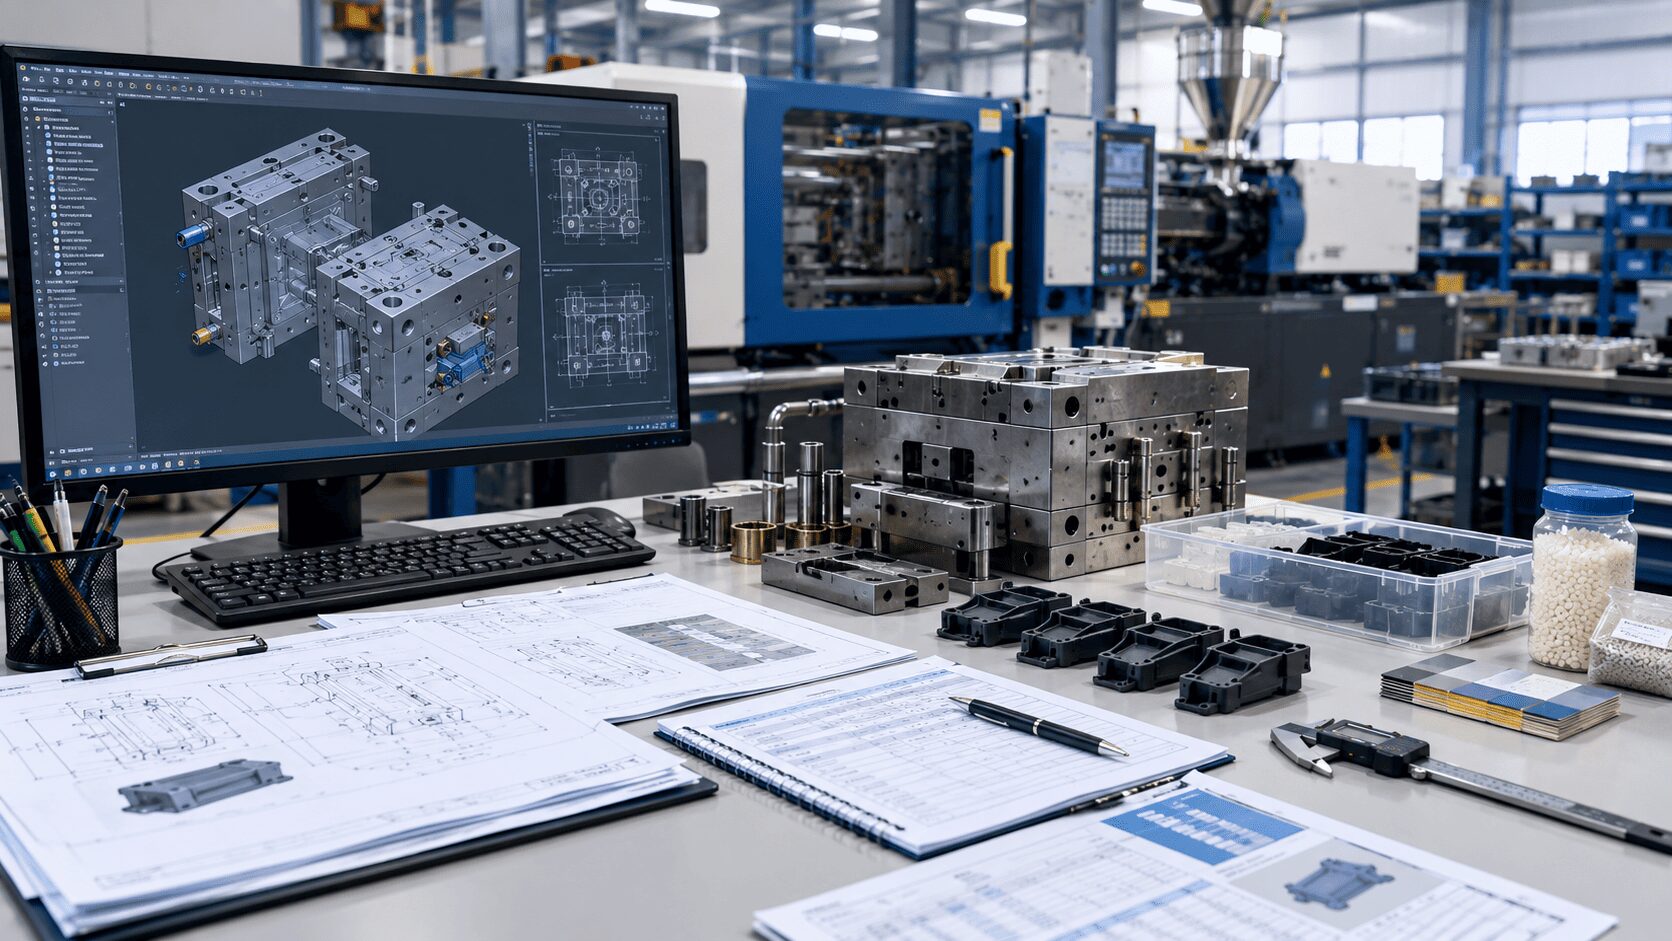
A molding trial is not simply the moment a new mold enters the press. It is the point where tooling, resin behavior, part geometry, process settings, and quality expectations meet under production conditions. Knowing how to plan molding trials before the machine is scheduled prevents expensive guesswork, protects the tool, and gives your team evidence that the part can be produced consistently.
For OEMs, product developers, and procurement teams, the goal is not to produce a few acceptable samples. The goal is to establish a repeatable process that delivers compliant parts at the required cycle time, volume, and cost. That requires a trial plan built around decisions, data, and accountability.
How to Plan Molding Trials Before the Tool Arrives
A successful trial begins well before mold installation. The mold designer, process engineer, quality team, and customer contact should agree on what the trial must prove. If the purpose is unclear, the team may spend valuable press time adjusting settings without knowing whether the result supports production approval.
Start by defining the trial stage. A first-off trial usually verifies basic mold function: filling, ejection, cooling, gate performance, and obvious cosmetic issues. A later trial should confirm dimensional capability, material performance, cycle time, repeatability, and assembly fit. Combining all objectives into an initial trial is possible for simple parts, but it can create confusion when a new tool needs mechanical adjustment before process validation can begin.
Set measurable objectives
Write the objectives as pass-or-fail statements. “Improve part quality” is too broad to guide a molding technician. “Achieve complete fill without flash at the defined cosmetic surfaces” is actionable. So is “hold the critical bore diameter within the specified tolerance over a documented production run.”
Define the required sample quantity and what each sample set will be used for. Some parts need samples for visual approval, dimensional measurement, functional testing, assembly testing, and customer review. Separate those requirements in advance. A small appearance sample may be enough for an early design review, while a production approval package may require parts from a stabilized process, traceable material, and a documented inspection plan.
Confirm the production inputs
The tool is only one variable. Confirm the approved resin grade, color, additive package, moisture specification, and drying requirements. Resin substitutions can alter shrinkage, flow, surface finish, weld-line strength, and cycle time. If a customer expects production in a specific material, trialing with a convenient alternative may provide misleading results.
The molding machine must also suit the tool and the process. Check clamp-tonnage demand, shot-size range, tie-bar spacing, mold height, nozzle interface, hydraulic or electric machine requirements, and auxiliary equipment. For parts with tight tolerances or demanding cosmetic standards, temperature control, material handling, and mold cooling capacity deserve the same attention as the press itself.
Build a Trial Plan Around Controlled Variables
A trial should produce useful data, not a collection of settings changed too quickly to interpret. Establish a baseline process first. Record melt temperature, mold temperature, injection speed profile, transfer point, packing pressure and time, cooling time, back pressure, screw speed, clamp force, and total cycle time.
Then change one meaningful variable at a time, unless a specific process issue requires a planned combination of adjustments. When short shots, sinks, warpage, or flash appear, the team needs to know whether the cause was pressure, temperature, fill rate, venting, cooling, or tool geometry. Uncontrolled changes make root-cause analysis slower and can hide a tooling correction that is actually required.
For every trial, the documented plan should identify at least these four elements:
- The starting process window and the permitted adjustment range for each critical setting.
- The samples to retain, label, and inspect after each condition is tested.
- The acceptance criteria for dimensions, appearance, weight, function, and assembly.
- The decision owner for tool changes, process changes, and customer approvals.
A process window is especially valuable because an acceptable part made at one narrow setting is not necessarily production-ready. The trial should test whether quality remains stable within realistic operating limits. A part that only passes at an unusually slow cycle or at maximum injection pressure may require mold refinement before full production can be committed.
Inspect Parts With Production in Mind
Visual inspection is necessary, but it cannot be the only measure of a successful molding trial. Define critical-to-quality features directly from the drawing, CAD model, customer specifications, and functional requirements. Typical priorities include mating surfaces, holes and threads, sealing features, snap fits, wall-thickness transitions, flatness, and appearance zones.
Measure parts after sufficient conditioning when the material requires it. Some polymers continue to shrink or absorb moisture after molding, so measurements taken immediately at the press may not represent the final state. The inspection method should be appropriate for the tolerance. A hand caliper may be adequate for an early check, while a critical sealing diameter or complex profile may need a coordinate measuring machine, gauges, or functional fixtures.
Look beyond individual dimensions
A part can meet each isolated dimension yet fail in assembly. Include functional checks whenever possible: insert a mating component, test a latch, verify torque, check a seal, or place the part in a fixture that represents the final application. This is particularly relevant for automotive, electrical, water-management, and automation components, where a minor variation can affect safety, leakage resistance, or downstream assembly time.
Track part weight as well. Weight variation can expose inconsistent fill, packing, or material delivery before a visible defect develops. When paired with dimensional and cosmetic data, it gives the process engineer a faster view of whether the molding process is stabilizing.
Separate process issues from tooling issues
Not every defect should be corrected through machine settings. Flash may point to excessive pressure, but it can also indicate a mold mismatch or damaged shutoff. Sink marks can respond to pack adjustments, but poor gate location or insufficient local wall support may be the underlying limitation. Warpage may be improved through cooling balance, yet the part design and gate strategy may need review.
This distinction matters because temporary process workarounds often increase cycle time, scrap risk, or maintenance demand. In-house mold modification capability is valuable here: the tooling and molding teams can review evidence together, make targeted corrections, and return to the press without the delay of sending the mold to an outside shop. At Glasfil, that integrated control supports faster decisions from initial trial through production release.
Plan Time for Corrections and Re-Trials
A realistic schedule treats the first trial as a controlled learning stage, not a final approval date. Reserve time for part inspection, customer feedback, tool adjustments, and a follow-up run. The amount of contingency depends on part complexity, resin behavior, tolerance requirements, number of cavities, and the maturity of the design.
Simple open-and-shut tools with established materials may need only limited refinement. Multi-cavity molds, tight-tolerance components, complex slides, textured surfaces, or parts with strict appearance requirements usually benefit from phased trials. Pushing for approval before the process is stable can move the cost downstream into sorting, field issues, delayed launches, and emergency tool changes.
Define how changes will be controlled. Each modification should be recorded with the reason, location, date, responsible owner, and expected impact. After a tool change, repeat the specific checks affected by that change rather than assuming prior results still apply. This traceability creates a useful history for future maintenance and repeat programs.
End the Trial With a Clear Production Decision
The final trial review should answer a practical question: can this mold now run the required part reliably at the agreed quality level and production rate? Review process settings, cycle time, inspection results, sample status, open issues, and any remaining tool work. If approval is conditional, document the conditions precisely.
A strong handoff includes the validated process sheet, resin and drying instructions, mold-temperature requirements, inspection criteria, approved sample reference, packaging needs, and maintenance notes. These details protect repeatability when production shifts, volumes increase, or the tool returns after service.
Well-planned molding trials shorten the path to dependable production because they replace opinions with evidence. Give the team a defined objective, a controlled process, and authority to act on the results, and the trial becomes a production decision rather than a costly experiment.
Contact us to discuss your project, request a quotation, or arrange a technical consultation. Our team will help you determine the most cost-effective and reliable way to manufacture your part.