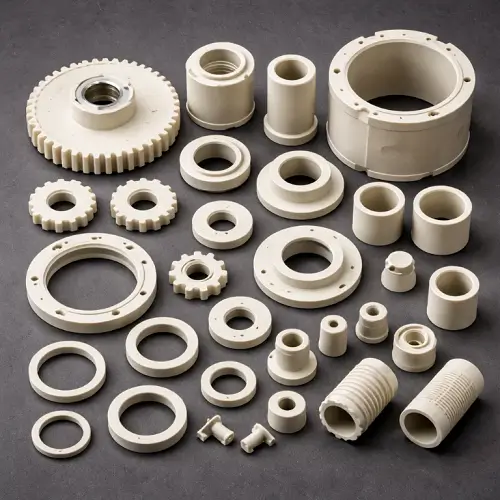
A water meter housing that passes a short pressure test but creeps out of tolerance after years in chlorinated water is not a successful part. Selecting the best resins for water meters requires more than comparing tensile strength or resin price. The material must match the meter’s pressure class, water temperature, chemical exposure, potable-water requirements, sealing geometry, production volume, and molding process.
For OEMs and product teams, the most reliable choice is usually a qualified resin grade paired with a part design that respects what the material can do over time. Resin families matter, but the specific grade, reinforcement package, stabilization, regulatory documentation, and processing window matter just as much.
What Water Meter Resin Must Withstand
Water meter components operate in a demanding environment. Even a standard residential cold-water meter may see continuous internal pressure, temperature cycling, dissolved minerals, disinfectants, installation stress, and long periods under load. Smart meter designs add electronic enclosures, transparent reading windows, sensor mounts, battery compartments, and tamper-resistant features.
The first distinction is between the wetted pressure-bearing body and secondary components. A material suitable for a protective register cover may be completely unsuitable for a threaded meter body or a valve-adjacent component. The body must retain dimensional stability around ports, threads, seal grooves, and metal inserts. It also needs sufficient long-term creep resistance so gasket compression and connection geometry remain controlled.
For potable-water applications in the US, material selection should begin with the required approvals. Depending on the component and the system requirements, suppliers may need to provide evidence of compliance with NSF/ANSI/CAN 61 for drinking-water system components and NSF/ANSI 372 for weighted lead content. Approval is grade-specific. A base polymer name is not proof that every formulation within that family is acceptable for potable water contact.
Best Resins for Water Meters by Application
Glass-Filled Nylon 66 for Pressure-Bearing Housings
Glass-filled PA66 is often a strong candidate for water meter bodies, connection elements, structural frames, and high-load covers. It provides high stiffness, good strength, practical moldability, and an established supply base. With the right grade, it can support complex injection-molded geometries that would be expensive to machine or assemble from several parts.
Its main advantage is the balance between mechanical performance and manufacturing efficiency. Glass reinforcement improves stiffness and reduces shrinkage, which is valuable for controlling threaded interfaces, O-ring grooves, and features that locate brass or stainless inserts.
The trade-off is moisture absorption. Nylon absorbs water, and that changes dimensions and mechanical behavior. A design team must account for conditioned dimensions, not just dimensions measured immediately after molding. Hydrolysis resistance also requires close review where hot water, elevated chlorine exposure, or prolonged thermal cycling is expected. For cold-water meter bodies, a hydrolysis-stabilized, potable-water-approved glass-filled PA66 grade can be a practical production choice. For more severe service, it may not provide enough long-term margin.
PPS for Hot Water and Aggressive Service
Polyphenylene sulfide, or PPS, is a premium option when heat, chemical resistance, low moisture absorption, and dimensional stability are central requirements. Glass-filled PPS is well suited to demanding meter housings, manifolds, sensor carriers, and internal fluid-handling parts where conventional engineering resins may lose performance.
PPS retains its properties well at elevated temperatures and has excellent resistance to many chemicals. Its low water uptake also makes it attractive for precision sealing features and tight-tolerance assemblies. If a meter is designed for hot water, district heating-related applications, or harsh disinfectant conditions, PPS deserves early consideration.
The cost is higher material price and a less forgiving molding process. PPS compounds require disciplined mold-temperature control, appropriate tool steel selection, proper venting, and careful gate placement. Glass-filled grades can also be abrasive, so wear-resistant tooling and planned mold maintenance are part of the real program cost. The material is justified when its service-life advantages reduce warranty risk or enable a higher-performing product.
POM for Internal Moving and Precision Components
Polyoxymethylene, commonly called POM or acetal, is frequently used for internal components that benefit from low friction, good dimensional stability, and repeatable movement. It is a strong option for gears, impellers, bearing elements, flow-measurement components, clips, and certain valve-related parts, subject to the application’s regulatory and chemical requirements.
POM performs particularly well where a molded part must move smoothly without extensive lubrication. It also has low moisture absorption compared with nylon, which helps maintain precision in assemblies exposed to water.
However, POM should not be treated as an automatic choice for every wetted component. Compatibility with chlorinated water, temperature limits, pressure loading, and the relevant potable-water approval must be confirmed for the exact grade. It is generally more appropriate for functional internal parts than for highly loaded, large pressure housings.
Polycarbonate and Acrylic for Readable Covers
Transparent meter windows and register covers create a different material challenge. The part must remain clear, resist impact, and survive outdoor exposure when the meter is installed above ground or in a sunlight-exposed enclosure.
Polycarbonate offers high impact resistance and is useful for protective covers, display windows, and smart meter housings. Acrylic provides excellent optical clarity and weathering performance but is more brittle than polycarbonate. The right choice depends on whether impact resistance, optical appearance, chemical resistance, or UV durability carries the most weight.
Neither material should be selected from a data sheet alone. Cleaning chemicals, condensation, UV exposure, ultrasonic welding, and assembly stress can all affect transparent plastics. Gate location and mold finish also have a visible effect on the final part.
Polypropylene for Lower-Pressure and Nonstructural Parts
Polypropylene can be a cost-effective material for covers, protective caps, battery compartments, packaging-related components, and lower-pressure fluid parts. It has good chemical resistance and low density, and it processes efficiently in high-volume injection molding.
Its limitation is lower stiffness and weaker long-term load resistance than PA66 or PPS. A polypropylene body may be appropriate for a carefully designed low-pressure application, but it is not a substitute for a high-performance engineering resin where threaded connections, sustained pressure, or heat are involved. Reinforced polypropylene grades improve stiffness, though the resulting material still needs application-specific validation.
Resin Selection Must Start With the Meter Design
Choosing a material before defining the loads often leads to costly redesign. The better sequence is to establish the pressure rating, normal and peak water temperatures, expected service life, disinfectant chemistry, installation environment, and regulatory requirements. Then review the molded features that create risk: threads, weld lines, sharp corners, insert interfaces, thin sections, sealing lands, and snap connections.
For example, a residential cold-water meter with a reinforced polymer body may point toward stabilized glass-filled PA66. A compact hot-water meter with strict dimensional retention requirements may justify PPS. A precision impeller or gear may be better suited to POM, while a readable outdoor register cover may require UV-stabilized polycarbonate or acrylic.
This is also where part consolidation can create value. A redesigned housing may replace multiple assembled components with one molded part, but only if the chosen resin can fill the geometry without creating weak weld lines or unacceptable warpage. The least expensive resin per pound is not always the lowest-cost manufacturing solution.
Tooling and Processing Determine Final Performance
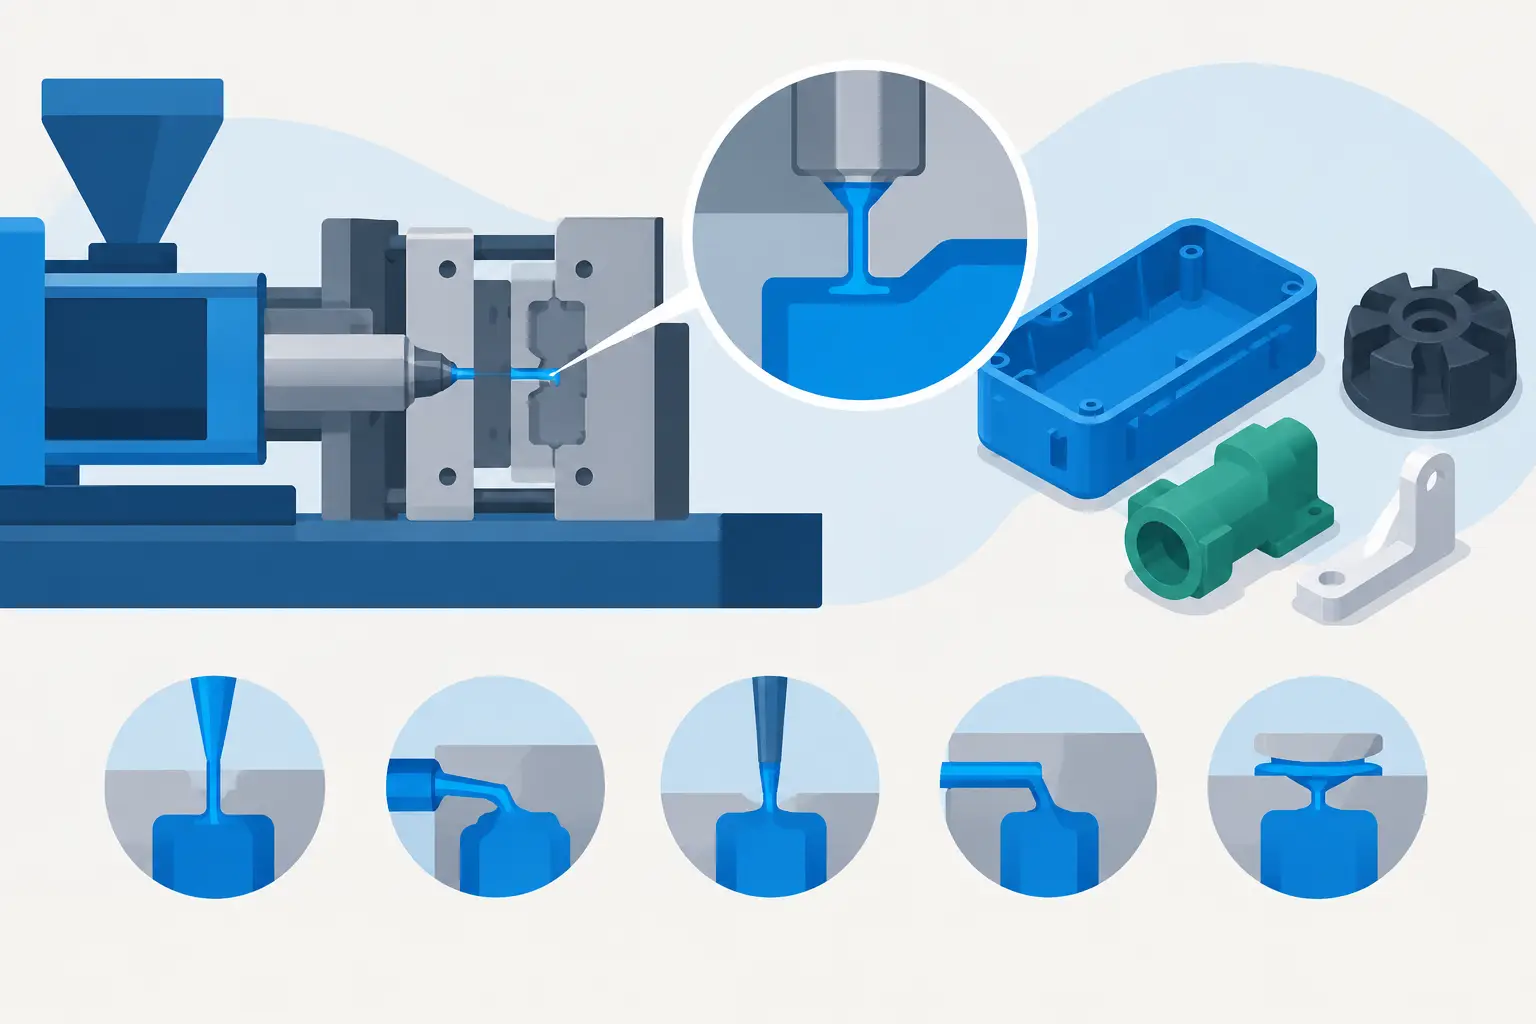
Even the right resin can fail in production when the mold and process are not built around it. Fiber-filled compounds create directional shrinkage, and that can distort circular interfaces or shift critical dimensions. Gate placement, flow path, cooling balance, venting, and ejection all influence part quality.
For pressure-bearing meter parts, engineering teams should pay particular attention to knit lines near ports and threaded features, sink around heavy sections, and stress concentrations at transitions. Uniform wall thickness, generous radii, and properly designed ribs reduce molding stress and improve consistency. Metal inserts require controlled preheating and geometry that avoids splitting the surrounding plastic during installation or field use.
A capable manufacturing partner should review material behavior alongside mold design, not after tooling is complete. Glasfil supports this work through in-house mold design, fabrication, molding, modification, and quality control, allowing design changes to be resolved without handing the project through multiple suppliers.
Validate the Grade, Not Just the Polymer Family
A material callout such as “30% glass-filled nylon” is incomplete for a water meter program. The final specification should identify the approved grade, color or pigment requirements, certification needs, conditioning requirements, and critical mechanical properties. It should also define what must be tested after molding.
Validation commonly includes hydrostatic pressure testing, leak testing, dimensional inspection after conditioning, torque testing at threaded connections, thermal cycling, chlorine or disinfectant exposure where applicable, and assembly testing with the intended seals and inserts. Long-term testing is especially valuable when the product relies on plastic threads or sustained gasket compression.
Production controls should follow the same priorities. Material drying, lot traceability, process monitoring, inspection gauges, and documented acceptance criteria protect repeatability from the first samples through repeat production runs. Water meter performance is built into the process, not inspected into the finished part.
The right resin decision gives the design team room to manufacture consistently, meet potable-water obligations, and control lifecycle risk. Start with the actual service conditions, qualify the exact grade, and make tooling decisions with the resin’s long-term behavior in mind. That approach produces water meter components that remain accurate, sealed, and dependable long after the first pressure test.
Contact us to discuss your project, request a quotation, or arrange a technical consultation. Our team will help you determine the most cost-effective and reliable way to manufacture your part.