A finished molded part can look correct, pass dimensional inspection, and still create a serious quality exposure if no one can confirm which resin lot produced it. For automotive, electrical, utility, and other regulated or high-volume applications, resin traceability systems turn material history into usable production control. They allow manufacturers to identify what entered the plant, where it was stored, how it was processed, and which parts may be affected if an issue is discovered later.
The value is not paperwork for its own sake. The value is faster decisions when a customer asks a question, a supplier issues a material notice, or a defect trend appears after shipment. A well-designed traceability process narrows the scope of investigation, protects acceptable inventory, and prevents a small material issue from becoming a broad production disruption.
What Resin Traceability Means on the Shop Floor
Resin traceability is the ability to connect every production batch to the specific raw material information used to make it. At minimum, that usually includes the resin manufacturer, grade, color or additive designation, supplier lot number, receiving date, internal inventory location, drying or conditioning record where applicable, molding machine, production date, mold, operator or shift, and finished-part batch.
For some programs, the record must go further. Customers may require certificates of analysis, compliance declarations, regrind percentages, masterbatch lots, purge records, and packaging labels that preserve lot identity through shipping. Medical, automotive, electrical, and water-management components often have different documentation expectations. The right level of control depends on the application, customer requirements, production volume, and risk associated with part failure.
Traceability only works when the physical flow and the data flow match. If a resin bag is scanned at receiving but material is later transferred into an unmarked hopper, the system has created an administrative record without maintaining actual control. The process must follow the material from dock to finished goods.
Why Resin Lot Control Protects Production
Raw material variation is not always visible before molding. Moisture content, contamination, incorrect grade selection, color inconsistency, excessive regrind, or a supplier-side formulation issue can affect part strength, surface finish, dimensions, weld-line performance, electrical properties, and long-term durability.
Without material traceability, a quality team may need to quarantine every part made over several days or weeks while it determines the source of a problem. That can tie up inventory, delay customer deliveries, and create unnecessary sorting or replacement costs. With clear resin-to-production records, the team can isolate the machine runs and shipment lots connected to the suspect material.
This is especially relevant when one resin grade is used across several molds or when multiple approved lots are active at the same time. A molding operation may be producing similar black components from different material specifications. Visual checks alone will not reliably distinguish them. Controlled labeling, material verification, and accurate production records prevent an approved substitute, a similar grade, or the wrong additive package from entering the wrong job.
The Core Elements of Resin Traceability Systems
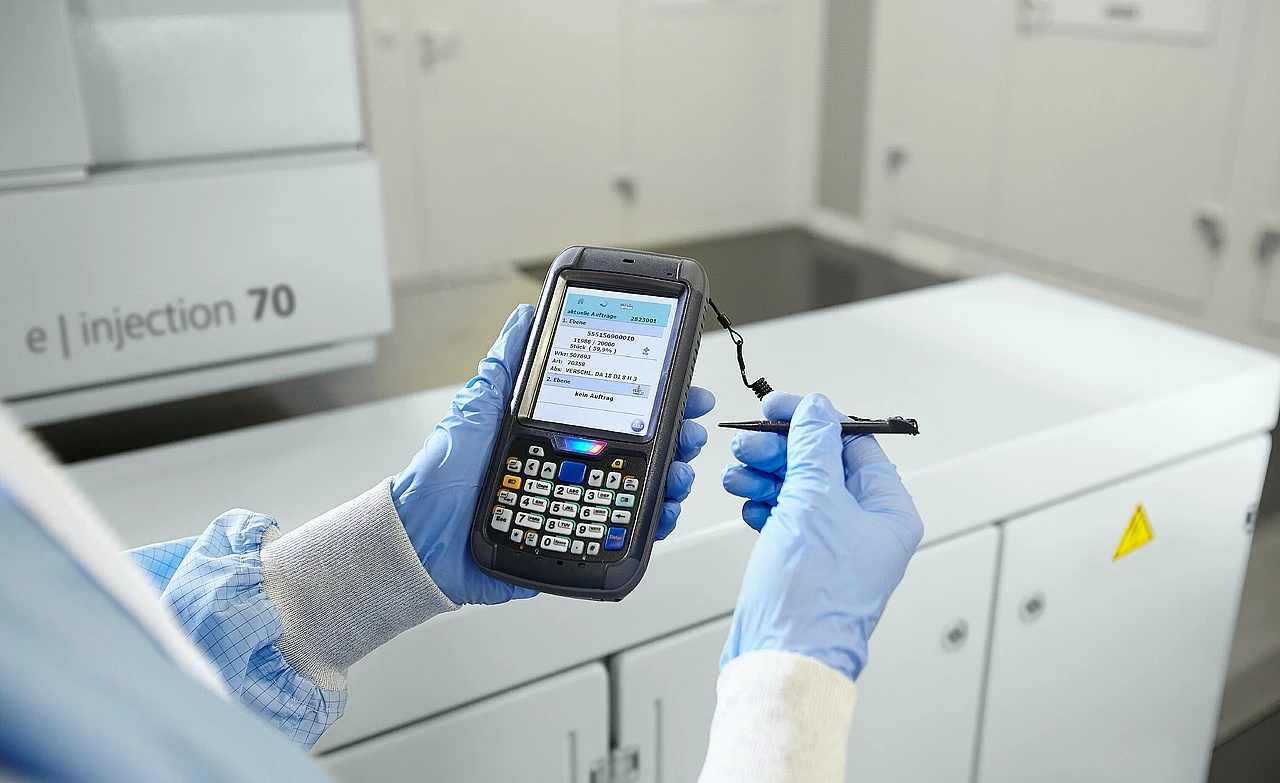
Effective resin traceability systems are built around disciplined material handling rather than a single piece of software. Barcode scanners, ERP platforms, manufacturing execution systems, and digital batch records can improve speed and accuracy, but they cannot correct unclear work instructions or uncontrolled material movement.
Receiving and material identification
Traceability starts when resin reaches the facility. Each pallet, gaylord, bag, or container should be checked against purchase documentation and labeled with its supplier lot number, internal material code, receipt date, and status. Material that has not passed receiving inspection should be clearly separated from approved inventory.
The receiving team also needs a defined process for retaining supplier documentation. When a customer asks for proof of resin grade or compliance, the record should be retrievable without searching through disconnected emails, paper files, and warehouse notes.
Controlled storage and issue to production
Once accepted, material must retain its identity in storage. Designated locations, labeled containers, first-in-first-out practices, and controlled material staging reduce the risk of mixed lots or unintended substitutions. For moisture-sensitive materials such as nylon, polycarbonate, PET, and certain filled compounds, drying records should connect to the material lot and production order.
When resin is issued to a molding machine, the production record should identify the specific lot used. If operators combine two lots in a hopper, that relationship must be captured. Otherwise, the system cannot accurately define the affected part population later.
Process and finished-goods linkage
Material data becomes useful when it is tied to actual manufacturing conditions. A complete production record can connect resin lot information with mold number, press number, cycle dates, process parameters, inspection results, and packing batch. This creates a chain from incoming material through shipped product.
Finished-goods labels should preserve enough information to identify the production batch after the parts leave the plant. The label format may use a work order number, date code, lot code, or serial sequence. What matters is that the code can be traced back quickly and consistently.
Choosing the Right Level of Traceability
Not every custom molded part requires the same system. Applying aerospace-level documentation to a simple, low-risk consumer component can add cost without improving the customer outcome. At the other extreme, relying on manual memory for a safety-related or performance-critical component creates avoidable exposure.
A practical approach begins with the customer specification and the consequences of failure. Consider whether the part is safety-related, installed in a regulated product, used outdoors for years, exposed to chemicals, or supplied to an OEM with formal containment requirements. Also consider production complexity. Traceability becomes more valuable when multiple resin suppliers, colorants, machines, plants, or subcontracted processes are involved.
Manual batch logs may be appropriate for short runs with limited material variation, provided they are complete, legible, and audited. Barcode-based records are often a stronger choice for repeat production and higher-volume programs because they reduce transcription errors. Integrated digital systems can provide the greatest visibility across receiving, molding, quality, and shipping, but they require disciplined implementation, staff training, and clean master data.
The best system is not necessarily the most complex one. It is the one that operators can follow under normal production pressure and that quality teams can rely on during an investigation.
Common Failures That Weaken Material Traceability
Many traceability gaps occur during routine activities rather than major process breakdowns. A hopper is topped off before the prior lot is recorded. A partial bag is moved to a different machine without a label. A color concentrate container is returned to storage with no lot identification. A production order is closed before all material usage is entered.
These issues are preventable when responsibilities are clear. Operators need simple instructions at the machine. Material handlers need a defined transfer process. Supervisors need to verify records before a job is released. Quality teams need regular checks that compare physical material labels with system transactions.
Regrind deserves particular attention. If regrind is permitted, the process should define which parts can be reground, the maximum allowable percentage, how regrind is labeled, and whether it may be used only within the same resin grade, color, and customer program. Uncontrolled regrind can compromise both material performance and lot traceability.
Building Traceability Into an Integrated Molding Program
For buyers, resin traceability should be evaluated as part of the wider manufacturing control plan. Material records are stronger when the same supplier manages mold design, tooling, molding, secondary operations, inspection, packing, and shipping. Fewer handoffs mean fewer gaps between material consumption, production records, and finished-goods identification.
At Glasfil, in-house tooling control and injection molding capability support this connected approach. When a part requires a mold adjustment, process correction, secondary operation, or quality review, the teams responsible can review the same production history rather than reconstructing it across separate suppliers. That helps contain issues quickly while keeping product launch and repeat-production schedules moving.
During supplier qualification, procurement teams should ask practical questions: Can the molder identify the resin lot used for a specific shipment? Can it identify all shipments made from a suspect lot? How are partial containers, colorants, and regrind controlled? How long are records retained? Can the supplier provide the documentation required by the customer’s quality system?
The answers reveal more than a software capability. They show whether the manufacturer has designed traceability into daily operations.
When a Material Issue Happens, Speed Matters
A traceability system proves its worth when there is a reason to use it. If a resin supplier notifies a molder of a potentially affected lot, the response should begin with immediate inventory status. The team must determine whether the material remains in receiving, storage, drying, machine hoppers, work-in-process, finished goods, or shipped product.
The next step is containment based on evidence, not assumptions. Production and shipment lots connected to the resin are placed on hold, while unaffected lots remain available where records support that decision. Quality teams can then review inspection results, process data, retained samples, and customer requirements to determine disposition.
That speed protects both sides of the supply chain. Customers receive clear information about scope and status. Manufacturers avoid stopping unrelated production. Most importantly, the organization can act before uncertain material becomes an uncertain field issue.
A traceable resin record is not just a quality document. It is a practical operating tool that gives manufacturers and customers the confidence to make the right decision when time is limited.
Contact us to discuss your project, request a quotation, or arrange a technical consultation. Our team will help you determine the most cost-effective and reliable way to manufacture your part.